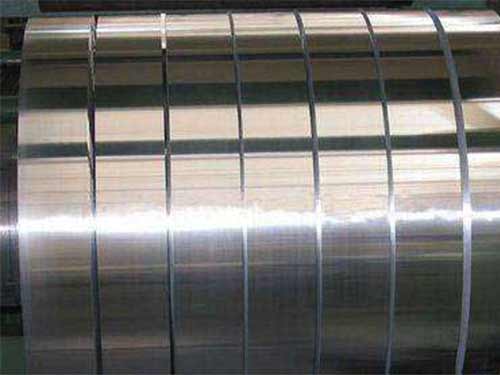
Mirror Laminated Aluminum Strip
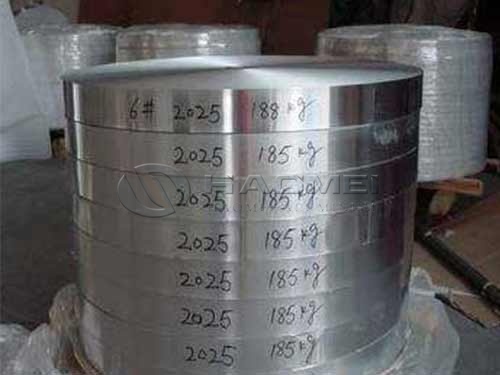
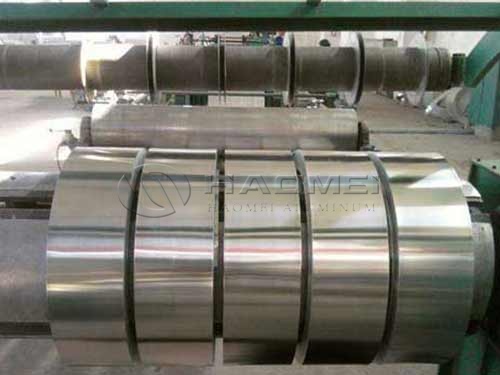
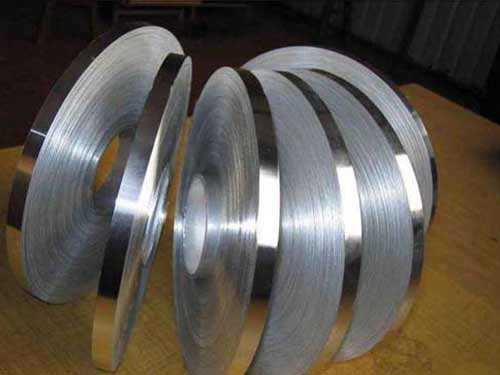
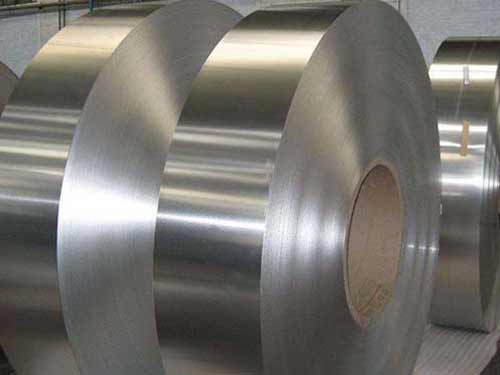
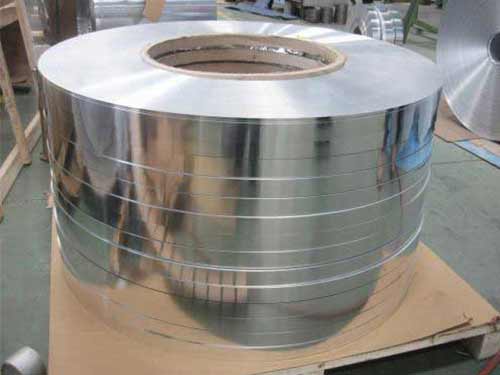
Mirror laminated aluminum strip is a precision-slit aluminum product with a bright mirror finish protected by a laminated surface film. It combines the light weight and formability of aluminum with a highly reflective appearance that remains protected during transport, fabrication, bending, stamping, and installation.
The product is commonly supplied in coils and slit strips for decorative trim, lighting reflectors, appliance panels, furniture edging, ceiling systems, signage, insulation jacketing, and selected electronic components. Depending on the intended environment, the base metal can be selected from commercially pure aluminum for superior reflectance or manganese-containing alloys for added strength and corrosion resistance.
Product Construction and Surface Concept
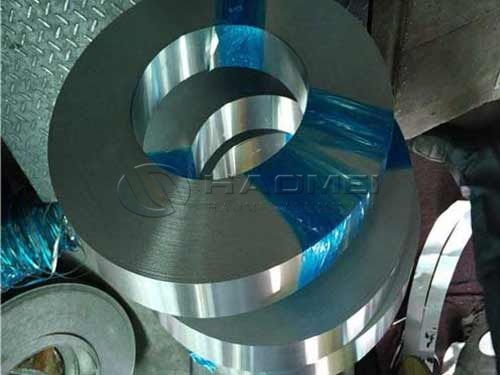
A mirror laminated aluminum strip generally consists of an aluminum substrate, a mechanically polished or chemically brightened reflective surface, and a transparent protective film. The laminate may be a temporary peelable film used during fabrication, or a functional clear film intended to remain on the finished part.
| Layer | Typical Material | Primary Function |
|---|---|---|
| Aluminum substrate | 1050, 1060, 1100, 3003, 3105, or 5052 alloy | Provides formability, stiffness, conductivity, and low weight |
| Mirror face | Rolled, polished, anodized, or bright-finished aluminum | Produces high visual brightness and light reflection |
| Laminated film | PE, PVC, PET, or specialty protective film | Reduces scratches, fingerprints, abrasion, and handling damage |
| Optional adhesive system | Pressure-sensitive or heat-activated adhesive | Bonds permanent film layers when required |
The protective film is especially valuable where the strip passes through roll forming, press brakes, stamping dies, or assembly fixtures. It helps preserve the reflective surface until the component reaches final installation. Film thickness, adhesion level, and peel behavior can be selected according to forming severity and temperature exposure.
Material Grades and Chemical Composition
Commercially pure alloys are often selected for reflector and decorative applications because they offer excellent brightness, soft temper options, and stable forming behavior. Alloyed grades such as 3003 or 3105 are preferred when a stronger strip is needed for trim profiles, panels, and semi-rigid fabricated parts.
| Alloy | Al | Mn | Mg | Si + Fe | Cu | Typical Use Direction |
|---|---|---|---|---|---|---|
| 1050 | 99.50% min. | ≤0.05% | ≤0.05% | ≤0.40% | ≤0.05% | High-reflection and decorative parts |
| 1060 | 99.60% min. | ≤0.03% | ≤0.03% | ≤0.35% | ≤0.05% | Lighting, appliance, and formed trim |
| 1100 | 99.00% min. | ≤0.05% | ≤0.05% | ≤0.95% | 0.05-0.20% | General bright-finish fabrication |
| 3003 | Balance | 1.0-1.5% | ≤0.05% | ≤0.70% | 0.05-0.20% | Stronger decorative and industrial strip |
| 3105 | Balance | 0.30-0.80% | 0.20-0.80% | ≤0.60% | ≤0.30% | Coated trim and formed panel systems |
Values are typical alloy limits and may vary with the governing standard, order specification, and production route. For applications requiring enhanced strength with a bright laminated face, 3003 Aluminum Strip is a practical material option.
Technical Specifications
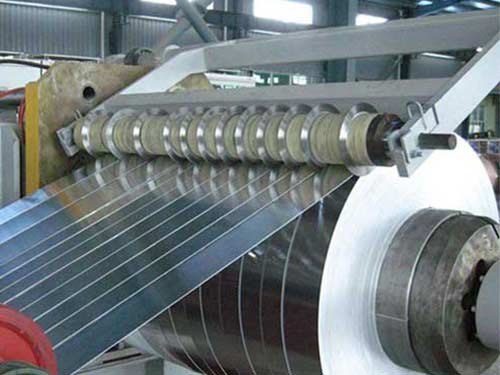
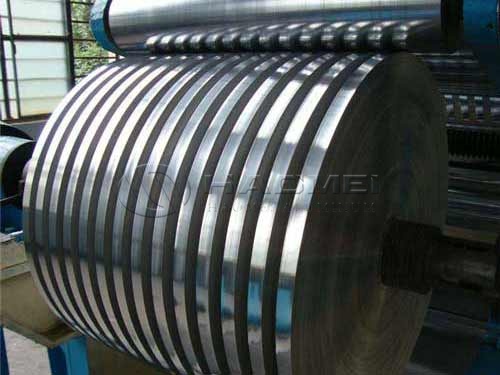
Mirror laminated aluminum strip can be tailored to match automated production lines and finished-part dimensions. Narrow slit coils reduce customer-side cutting losses, while wider stock supports progressive blanking and panel fabrication.
| Parameter | Common Supply Range | Notes |
|---|---|---|
| Thickness | 0.20-2.00 mm | Thinner gauges suit reflectors and edging; heavier gauges suit trim and panels |
| Width | 10-1,600 mm | Narrow widths are available as slit coils |
| Coil inner diameter | 150 mm, 300 mm, 400 mm, 500 mm | Selected to match decoiler equipment |
| Coil outer diameter | Up to 1,800 mm | Controlled by weight and handling limits |
| Coil weight | 100-5,000 kg | Available in lightweight or mill-scale coils |
| Temper | O, H12, H14, H16, H18, H22, H24 | Temper affects bendability, flatness, and springback |
| Mirror finish | Standard bright to high-reflective | Surface quality should be agreed using samples |
| Protective film thickness | 30-100 μm | PE and PVC films are common for temporary protection |
| Film adhesion | Low, medium, or high tack | Matched to forming depth and removal conditions |
| Edge condition | Mill edge, slit edge, deburred edge | Slit-edge quality is important for safe handling |
Mechanical and Functional Performance
Mechanical properties depend on alloy, thickness, temper, and the direction of rolling. Soft tempers are well suited to deep bends and shaped profiles, while H14 and H24 tempers provide a balanced combination of strength and manufacturability.
| Alloy and Temper | Tensile Strength | Yield Strength | Elongation | Forming Character |
|---|---|---|---|---|
| 1050 O | 60-95 MPa | 20-35 MPa | 25% min. | Very suitable for bending and drawing |
| 1060 H14 | 95-135 MPa | 75-120 MPa | 3-12% | Balanced rigidity and simple forming |
| 1100 H14 | 110-145 MPa | 95-125 MPa | 4-10% | Suitable for decorative profiles |
| 3003 H14 | 145-185 MPa | 115-160 MPa | 3-10% | Higher strength for formed components |
| Performance Aspect | Expected Result | Customer Value |
|---|---|---|
| Reflectivity | Bright, mirror-like visual effect | Enhances lighting efficiency and decorative impact |
| Surface protection | Film limits handling scratches and marks | Reduces reject rates during fabrication |
| Corrosion behavior | Aluminum naturally forms a stable oxide layer | Suitable for many indoor and sheltered outdoor uses |
| Weight | About one-third the density of steel | Easier handling and lower structural load |
| Thermal conductivity | High for pure aluminum grades | Supports heat-spreading and reflector uses |
| Recyclability | Fully recyclable aluminum substrate | Supports material recovery goals |
Applications That Benefit From a Mirror Face
In lighting equipment, mirror laminated aluminum strip is used for reflector channels, LED lamp housings, luminaire trim rings, and optical interior components. The bright face helps direct available light, while the film protects the appearance during cutting and assembly.
In architectural and interior finishing, the strip can be formed into decorative borders, elevator trims, cabinet edges, ceiling accessories, display frames, and wall-panel details. Its low mass makes long profiles easier to process than comparable stainless steel parts.
Appliance producers use bright laminated strip for refrigerator trim, cooker hood details, small appliance housings, control-panel borders, and ventilation grilles. The film can remain in place through stamping and be removed near final inspection, helping maintain a clean presentation surface.
For packaging machinery, transportation interiors, and instrument housings, alloy selection can be adjusted to prioritize strength, bend performance, or corrosion resistance. Customers requiring broader alloy choices can also consider Alloy Aluminum Strip for demanding formed components.
Processing Guidance
Protective film should remain on the mirror face as long as possible. Use clean rollers, non-marking guides, and polished tooling to prevent pressure lines or trapped debris. When bending laminated strip, select a bend radius appropriate for the alloy and temper; harder tempers generally require a larger radius to avoid edge cracking.
For temporary films, removal should be performed at a moderate and consistent angle after fabrication. Excessive heat, prolonged ultraviolet exposure, or storage in humid conditions may change adhesive behavior. Permanent laminated films should be evaluated for adhesion, color stability, chemical resistance, and heat exposure in the final service environment.
Value for Fabricators and Designers
Mirror laminated aluminum strip delivers a polished visual finish without the weight penalty of steel-based alternatives. Its protected surface can lower handling damage, reduce secondary polishing work, and improve consistency across high-volume parts. With suitable alloy, temper, slit width, and film selection, the material supports efficient coil-fed production while providing a bright finished appearance that customers notice immediately.
For reliable results, purchase specifications should define alloy, temper, thickness tolerance, width tolerance, surface reflectivity expectation, film type, adhesion level, coil dimensions, and permitted surface defects. A sample approval process is recommended when the finished part has demanding visual requirements.